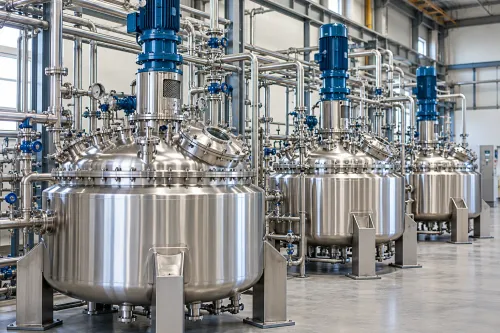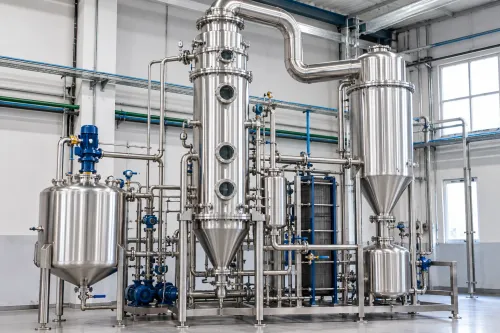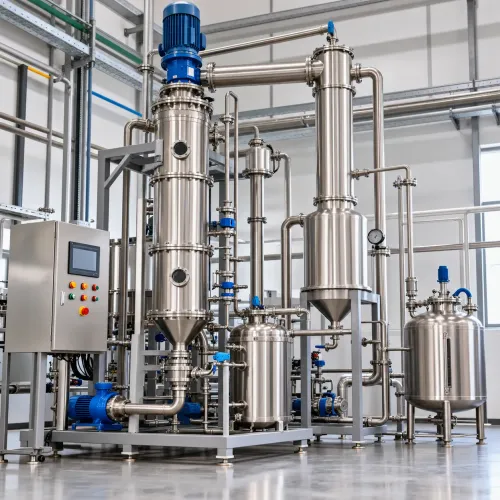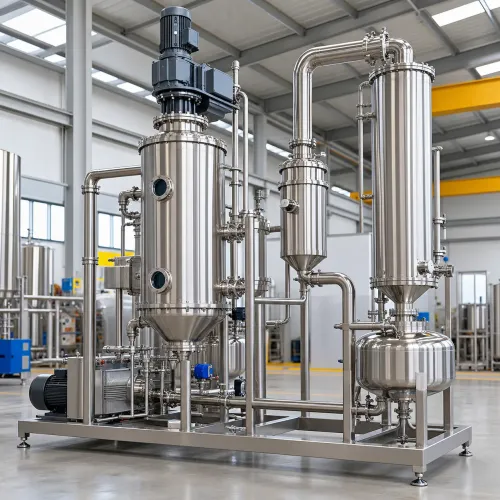
Industrial production frequently involves concentrating liquids, recovering solvents, or reducing wastewater volumes. These processes require reliable thermal equipment capable of operating efficiently under demanding conditions. Working with an experienced Multiple Effect Evaporator Manufacturer in Vadodara helps industries implement systems that support productivity while optimizing energy usage.
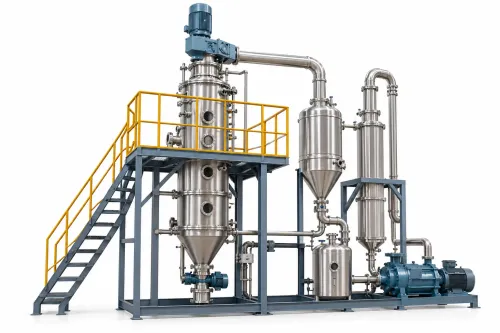
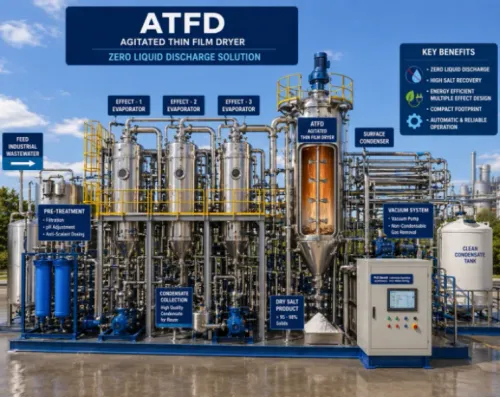
A Multiple Effect Evaporator uses a sequence of interconnected evaporation chambers, known as effects, where steam energy is reused multiple times. Instead of relying on fresh steam for every stage, the vapor generated from one effect becomes the heating medium for the next. This approach significantly lowers steam consumption and operating costs.
The technology has become increasingly popular because manufacturers seek better energy efficiency without compromising production capacity. As industries continue to focus on sustainability and operational optimization, multiple effect evaporators remain a preferred solution across several sectors.
Common applications include:
- Chemical concentration
- Pharmaceutical formulation processing
- Effluent treatment
- Solvent recovery
- Food ingredient concentration
- Distillery wastewater management
- Dye and pigment manufacturing
Different industries require different evaporator configurations. Factors such as product viscosity, scaling tendency, boiling point elevation, solids content, and corrosion potential influence equipment design. This is why engineering customization plays an important role during project planning.
One of the primary benefits of multiple effect evaporation is reduced energy consumption. By utilizing steam more efficiently, businesses can lower utility costs while maintaining production throughput. Over the lifespan of industrial equipment, these savings can represent a substantial return on investment.
Another advantage is improved environmental performance. Reduced steam usage lowers fuel consumption, while efficient evaporation systems help decrease wastewater volumes. These benefits support industries working toward stricter environmental regulations and resource conservation initiatives.
When selecting an equipment manufacturer, businesses should evaluate technical capabilities rather than focusing exclusively on pricing. Important considerations include:
- Process design expertise
- Heat transfer calculations
- Equipment fabrication standards
- Automation capabilities
- Material selection
- Performance testing
- Service support after installation
Many modern evaporators also include intelligent monitoring systems that provide real-time operating data. Operators can monitor temperatures, vacuum levels, steam pressure, and product concentration to maintain stable operating conditions. Automated controls reduce human error while improving production consistency.
Vadodara continues to serve as one of India's leading industrial engineering centres. Its strong manufacturing ecosystem has encouraged the development of specialized equipment suppliers serving chemical, pharmaceutical, and industrial processing sectors throughout Gujarat and beyond.
Another factor worth considering is maintainability. Industrial equipment should allow easy inspection, cleaning, and servicing without excessive production downtime. Well-designed evaporators simplify maintenance activities while helping facilities maintain higher equipment availability.
Chemie Prozessors manufactures evaporation systems by integrating process engineering with application-specific equipment design. The company's approach focuses on understanding individual production challenges before recommending suitable evaporation technologies for different industries.
As manufacturing operations continue to prioritize efficiency and sustainability, investing in properly engineered evaporation equipment becomes increasingly important. Selecting a knowledgeable Multiple Effect Evaporator Manufacturer in Vadodara allows businesses to improve process efficiency, reduce energy consumption, enhance product quality, and support long-term operational reliability through well-designed thermal processing solutions.
Keywords